
A holiday order can look small at checkout and still consume the one part of your shop that’s already full. Ten more ornaments may need little material but an hour of proof review. A sign may cut quickly but wait behind a week of sanding and finishing. A batch of printed gifts may clear the machine and then stall at inspection or packing.
That’s why “How many orders can I take?” is usually the wrong first question. Orders aren’t equal. The useful question is:
How many hours remain at the step that limits this order, after work you already promised and a realistic allowance for known rework?
This guide gives you a weekly capacity worksheet for answering that question. It isn’t a holiday demand forecast, a carrier deadline calendar, or a universal Christmas start date. And it won’t guarantee that every job goes perfectly. What it will do is help you stop treating an open square on the calendar as proof that the shop can absorb another promise.
Count the constraint, not the order total
A shop can have spare laser time and no finishing capacity. It can have an open printer and no trained operator time for file preparation. It can have finished products waiting because packing is the slowest stage. Total machine hours hide those differences.
Start by naming the bottleneck for the product family you’re considering. It may be:
- proofing and file preparation;
- machine setup or supervised run time;
- sanding, cleaning, curing, finishing, or assembly;
- inspection of personalized records;
- packing, labeling, or local-pickup preparation; or
- one trained person who must perform several of those steps.
The bottleneck is the step that limits how much acceptable work can leave the system during the promise window. It may change by product or by week. A laser can be the constraint for a large engraving run while hand-finishing is the constraint for signs. Don’t average unlike stages into one comfortable-looking number.
If two stages are tight, run the worksheet for both. The order fits only if it fits every required constraint. Adding machine hours won’t solve a packing bottleneck, and adding weekend packing time won’t create more supervised machine capacity.
Define the promise window before doing the worksheet
Use one row per real working week between now and the shop’s internal completion or handoff date. The internal date is when your controlled work must be complete. It isn’t a prediction about a carrier’s performance.
For each week, mark the actual windows when the bottleneck is available. Exclude days the shop is closed, market days, appointments, known maintenance, staff absences, and time already reserved for non-order work that can’t move. Count only staffed, safe, usable windows. Don’t turn every waking hour into capacity, and don’t assume equipment can operate without the supervision its manufacturer and your shop procedures require.
This is a production promise worksheet. Customer approval, material receipt, and any outside service can still determine when work becomes ready. If one of those inputs is unresolved, label it as a gate rather than quietly assuming it arrives on time.
Step 1: Find usable bottleneck hours
For each week, begin with scheduled hours at the constrained step. Then remove time that isn’t honestly available for new order work.
A simple line is:
Usable bottleneck hours = staffed bottleneck windows − protected non-order time
Protected time can include routine cleanup, required maintenance, a scheduled market, purchasing, or an existing operational obligation. Keep the list specific. “Admin” is too vague if it becomes a number you change whenever you want an order to fit.
Use observed time where possible. Review recent batches, time records, machine logs, packing sessions, or calendar blocks. If you’ve got no evidence for a new process, don’t borrow a throughput claim from another shop. Mark the estimate low-confidence, test the process before promising volume, or offer a smaller scope.
Capacity isn’t the fastest run you’ve ever completed. It’s the work you can repeat under the conditions that will actually exist that week.
Step 2: Convert accepted orders into committed workload
Next, list every order you’ve already accepted that uses the bottleneck during the worksheet window. Include work that hasn’t reached production yet.
For each commitment, record:
- order or batch ID;
- product and quantity;
- current gate, such as waiting for proof, approved, or in production;
- internal completion week;
- bottleneck step;
- setup time;
- per-batch or per-unit bottleneck time based on comparable work;
- inspection, handling, or packing time at that same constraint; and
- confidence or source for the estimate.
An accepted order doesn’t disappear from capacity just because the customer hasn’t approved the proof. Place it in the week your promise currently requires, and flag the unresolved gate. If a late approval would force the work into another week, show that scenario explicitly. Don’t spend the same hours on a new order while assuming the first customer will be late.
For personalized work, clean order status matters. The guide to batching personalized orders without spreadsheet chaos explains how to separate intake, proof, approval, production, and packing status. Use that order record as the source for committed work; this worksheet doesn’t replace it.
Add the bottleneck hours for all accepted work in each week. That total is your committed workload. Include setup and changeover where they consume the same constrained person or station. If two orders can truly share one setup, document the grouping once rather than charging both for the same time. Don’t assume they’ll batch together if their materials, files, approvals, or due weeks don’t support it.
Step 3: Reserve a buffer for rework you already know occurs
A zero-rework plan isn’t a capacity plan. It’s a best-case schedule.
Reserve time for the failures your own records show are plausible: a finish that needs correction, a damaged blank, an alignment remake, a mispacked personalized item, a failed quality check, or a file that must be re-exported. The allowance belongs in bottleneck hours, not only in spare materials.
Use recent comparable work to set it. You might review the last several batches in the same product family and total the actual bottleneck time spent on remakes, touch-ups, reinspection, and recovery. Then choose an allowance that reflects the evidence and current conditions. A newly changed process or material may justify more protection or a qualification hold; a stable repeat product may have better records.
Don’t copy a universal percentage from this article. Shops, products, and processes differ, and a percentage of unit count may not match hours at the constrained step. Record the basis beside the number, such as “recent ornament batches: observed rework and reinspection time” or “new finish: estimate uncertain; test required.”
Keep known existing rework separate from the allowance. If three pieces have already failed and you know they’ll need remaking, that’s committed work. The buffer protects against additional plausible recovery. It shouldn’t hide work that’s already real.
Step 4: Calculate protected remaining capacity
Now calculate each week’s protected remainder:
Protected remaining hours = usable bottleneck hours − accepted-order hours − known existing rework hours − additional rework buffer hours
A positive number isn’t automatically available for any order. It’s the maximum protected room at that constraint before considering the candidate order. Keep known remakes in their own line even if they are operationally part of committed work; that prevents them from disappearing inside a general allowance. Materials, approvals, other constrained stages, and product-specific uncertainty still matter.
A negative number is an escalation signal. The shop has already promised more constrained work than the current plan protects. Don’t accept another order just because its quantity looks small. Rework the existing schedule, simplify scope where customers agree, add only genuinely available qualified capacity, or communicate about affected commitments before selling more of the same constraint.
Don’t fill every protected remaining hour by default. Estimates with weak evidence need more caution than stable repeat work. Capacity that exists only if every approval arrives immediately or every batch hits its fastest observed time isn’t protected capacity.
A weekly holiday order capacity worksheet
Use one table for each bottleneck you need to test.
| Week | Usable bottleneck hours | Accepted-order hours | Known existing rework hours | Additional rework buffer | Protected remaining hours | Candidate-order hours | Remainder after candidate | Decision |
|---|---|---|---|---|---|---|---|---|
| Week 1 | Accept / revise / decline | |||||||
| Week 2 | Accept / revise / decline | |||||||
| Week 3 | Accept / revise / decline | |||||||
| Week 4 | Accept / revise / decline |
Attach two short ledgers so the totals remain auditable.
Committed-work ledger
| Order or batch | Required week | Bottleneck | Setup hours | Run/handling hours | Check/pack hours at bottleneck | Total committed hours | Estimate source/confidence |
|---|---|---|---|---|---|---|---|
Candidate-order card
| Field | Entry |
|---|---|
| Product, quantity, and approved scope | |
| Required internal completion or handoff date | |
| Ready-to-produce gates still open | |
| Bottleneck step or person | |
| Setup hours | |
| Production/handling hours at bottleneck | |
| Inspection/packing hours at bottleneck | |
| Comparable-job evidence | |
| Materials physically available or confirmed | |
| Week-by-week load | |
| Accept, revise, or decline | |
| Decision reason and reviewer/date |
The material line is a constraint check, not a reorder formula. If stock is the issue, use the Q4 inventory planning guide to review blanks, packaging, storage, and replenishment. Don’t count unconfirmed incoming stock as production capacity.
An illustrative decision across two weeks
Suppose a shop is testing a candidate order against finishing time, its current bottleneck. These figures are illustrative, not a benchmark for another shop.
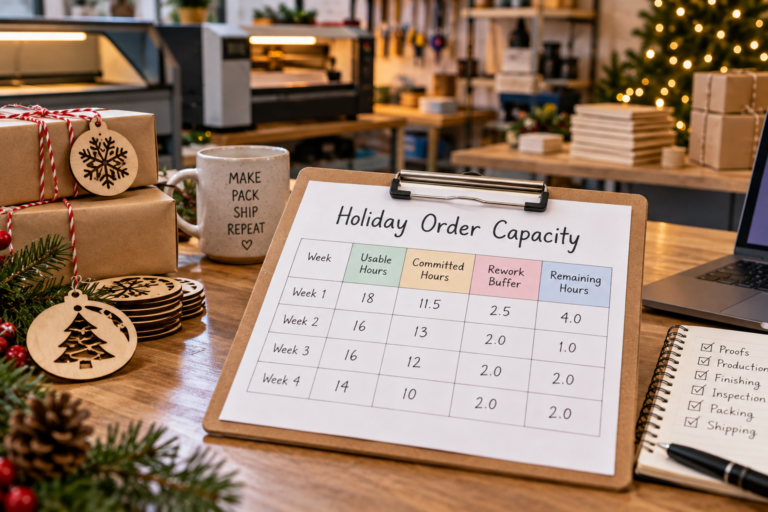
In Week 1, the shop has 18 usable finishing hours, 11.5 hours committed to accepted orders, and 2.5 hours reserved for evidence-based rework. That leaves 4 protected hours. If the candidate needs 3.25 finishing hours that week, 0.75 hour remains.
In Week 2, the shop has 16 usable hours, 13 committed hours, and a 2-hour rework allowance. Only 1 protected hour remains. If the candidate needs another 2.5 hours that week, the row falls to negative 1.5 hours.
The order doesn’t fit as promised, even though Week 1 looks positive and the total quantity may sound manageable. The shop could offer a smaller quantity that fits both weeks, move the internal completion date to a week with protected room, simplify the finish if the customer agrees and the new process is proven, or decline. It shouldn’t erase the buffer or borrow time already committed to make the answer look like yes.
Make the weekly accept, revise, or decline decision
Review the worksheet on the same day each week and whenever a large candidate order would materially change it. Reconcile estimates with actual bottleneck time before deciding what to offer next.
Accept when the candidate has a defined scope, its ready-to-produce gates are realistic, required materials are available or credibly confirmed, and every required bottleneck remains nonnegative in every affected week. Record the exact quantity, scope, internal date, assumptions, and hours consumed.
Revise when a defensible version can fit. Revisions may include fewer units, fewer variants, a later completion week, a proven simpler finish, staged quantities, or a ready-made alternative. Recalculate the revised order rather than assuming “smaller” means safe.
Decline when the order makes any required week negative, depends on unproven work under deadline, consumes a buffer the shop has evidence it needs, relies on materials that aren’t confirmed, or can fit only by risking promises already made.
This is different from deciding whether to sell rush service. If the request would jump the queue or compress the normal workflow, Laticy’s guide to rush orders for custom products covers eligibility, disruption, fees, and customer-facing terms. This worksheet answers the question that comes first: is protected capacity actually there?
Update the worksheet with actuals, not optimism
At the end of each week, replace estimates with what happened. Record:
- actual bottleneck hours used by each order;
- actual setup and changeover time;
- rework and recovery hours, with the reason;
- work moved into another week and why;
- unused windows that were truly available; and
- constraints that shifted to another step.
Don’t treat every unused hour as proof that the next week can take more. A window lost because files were late is different from spare production capacity. A bottleneck that moved from engraving to packing needs a new worksheet, not a larger sales target.
Over time, these records improve the estimates for products you repeatedly sell. They also show where operational changes might help. The point isn’t to squeeze the shop toward perfect utilization. The point is to make promises from visible workload instead of hope.
FAQ
Should I plan holiday capacity by orders, units, or hours?
Use hours at the bottleneck for the decision, then retain quantities and order IDs for traceability. Orders and units vary too much to show workload by themselves. Ten simple repeat items and ten proof-heavy personalized items may consume very different constrained time.
What if I don’t have reliable production-time records?
Mark the estimate low-confidence and gather evidence with a representative test or small controlled batch before promising volume. Use a smaller scope or later date when uncertainty is material. Don’t substitute another shop’s advertised speed for your complete workflow.
Does the rework buffer guarantee on-time completion?
No. It’s an allowance based on known, plausible recovery work, not a guarantee. Unusual failures, late approvals, unavailable materials, or other disruptions can still change the plan. Its purpose is to avoid a schedule that assumes zero friction.
Can I accept an order when one week goes negative but another week has spare hours?
Only if the work can genuinely move between those weeks without violating approvals, process sequence, material availability, existing commitments, or the promised scope and date. Move the load on the worksheet and check every affected constraint. Don’t borrow hours the process can’t actually use.
How often should I review holiday order capacity?
Use a consistent weekly review, then recalculate after a large acceptance, scope change, known remake, staffing change, or other event that materially changes the constrained workload. A decision recorded last week isn’t evidence that the same capacity remains today.
Holiday capacity isn’t the number of orders you hope to sell or the number of blank spaces on a calendar. It’s the protected time left at the step that controls completion. Count that time, subtract promises already made, protect a buffer based on known rework, and make the next acceptance decision week by week.